- Introduction
- Short Answer
- Working Principle: Energy and Power Answer Different Questions
- Worked Example: Three Loads on One Hot-Water Header
- Test the Schedule Before Taking Credit for It
- Convert the Peak into Hot-Water Flow
- Pump Head Comes from the Operating Network
- Cleaning Demand Needs Its Own Schedule
- What to Put in the Utility Design Basis
- Frequently Asked Questions (FAQ)
- Conclusion
- Sources
Introduction
On November 2, 2026, KHS announced an expansion of its Innoplant consultancy and engineering offering. The service connects early beverage-plant planning with detailed engineering, implementation, and lifecycle support. Its scope includes project-specific utility supply planning. This is a service announcement, not evidence of measured savings from a completed installation. (khs.com, khs.com)
The engineering implication is practical: utility requirements should be established alongside production sequences, before individual equipment selections become fixed.
In a batch plant, several machines may share hot water, steam, cooling water, or cleaning services. Adding their maximum ratings gives one number. Averaging their consumption gives another. Neither automatically identifies the required utility capacity.
This article develops a simple load schedule to show how timing affects the selection of a shared hot-water system.
Short Answer
Calculate utility demand against time and operating scenario.
Distinguish:
- Connected maximum load: the sum of individual maximum duties.
- Coincident peak demand: the greatest combined demand occurring in a defined scenario.
- Average demand: energy or consumption divided by the observation period.
Use the justified peak and temperature conditions to assess thermal capacity and circulation flow. Evaluate hydraulics separately to establish pump head, valve requirements, and pipe sizing.
Any capacity reduction based on sequencing depends on that sequence remaining credible.
Working Principle: Energy and Power Answer Different Questions
Heating a batch requires energy. Delivering that energy within a specified time requires power.
For an idealized sensible-heating calculation:
Energy = mass × specific heat capacity × temperature rise
Then:
Average heating power = energy ÷ heating time
The same batch can therefore require different heating rates depending on the permitted warm-up time.
Spirax Sarco’s steam-consumption guidance distinguishes batch and flow applications and explains why equal energy requirements do not imply equal heat-transfer rates. It also cautions that equipment ratings depend on operating conditions. (spiraxsarco.com)
A realistic assessment also considers equipment heating, losses, changing temperature differences, and achievable exchanger performance. Dividing energy by time establishes a mean requirement; it does not prove the equipment can maintain that rate throughout the batch.
Worked Example: Three Loads on One Hot-Water Header
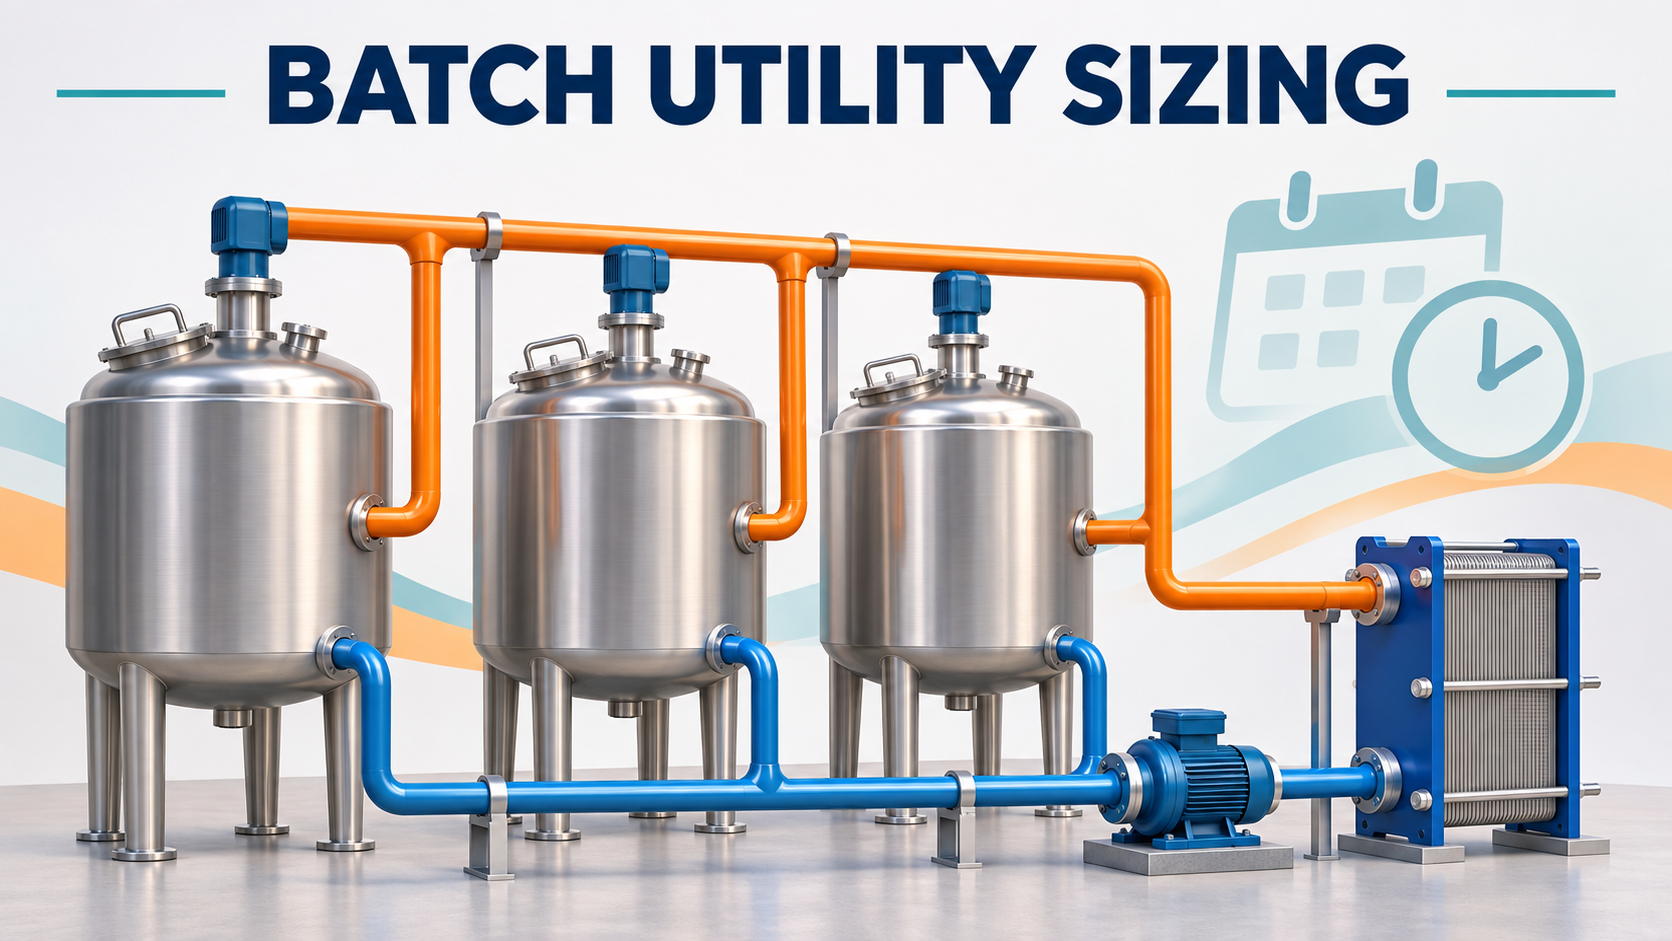
Consider three hypothetical users supplied by a common hot-water utility:
User
Assumed maximum thermal demand
A: Batch-tank heating
400 kW
B: Process-heating circuit
300 kW
C: Cleaning-solution heating
200 kW
Sum of individual maxima
900 kW
Now assume an approved operating sequence produces the following demands:
Time interval
User A
User B
User C
Combined demand
0–10 minutes
400 kW
300 kW
0 kW
700 kW
10–20 minutes
400 kW
0 kW
200 kW
600 kW
20–30 minutes
0 kW
300 kW
200 kW
500 kW
All values and timings are original teaching assumptions, not plant data or KHS specifications.
For this particular schedule:
Connected maximum load = 400 + 300 + 200 = 900 kW
Coincident peak demand = 700 kW
The energy consumed during the half-hour is:
700 × 10/60 + 600 × 10/60 + 500 × 10/60 = 300 kWh
Therefore:
Average demand = 300 kWh ÷ 0.5 h = 600 kW
The three answers serve different purposes:
Quantity
Result
What it describes
Connected maximum
900 kW
All individual maxima added
Scheduled peak
700 kW
Highest demand in this sequence
Half-hour average
600 kW
Energy use spread over the period
Selecting a 600 kW heat source solely from the average leaves an instantaneous shortfall during the first interval unless storage or another justified mechanism supplies it.
Conversely, 900 kW may exceed the scheduled requirement—but only if overlapping operation is genuinely prevented or otherwise accommodated.
Test the Schedule Before Taking Credit for It
A planned sequence is an assumption until its operating basis is established.
Review what happens when:
- A batch starts late and overlaps the next operation.
- Cleaning begins while production is recovering from a stoppage.
- Several cold units restart together.
- Operators use a permitted manual mode.
- Future production requires shorter turnaround times.
In the example, simultaneous operation of all three users would demand 900 kW.
A scheduling benefit should therefore be connected to documented constraints, control behavior, or an accepted operating limitation. An informal expectation that operators will avoid overlap is weak evidence for reducing installed capacity.
Also identify the consequences of exceeding available capacity. A longer heating time may be acceptable in one process and unacceptable in another.
Convert the Peak into Hot-Water Flow
Assume the shared utility transfers 700 kW with a 20 K water-temperature decrease across the active users.
For illustration, use:
- Specific heat capacity: 4.18 kJ/(kg·K)
- Density: 1,000 kg/m³
- Negligible distribution heat loss
The required mass flow is:
700 ÷ (4.18 × 20) ≈ 8.37 kg/s
The corresponding volume flow is:
8.37 ÷ 1,000 × 3,600 ≈ 30.1 m³/h
At 900 kW with the same assumed temperature change, the equivalent flow would be approximately 38.8 m³/h.
This calculation establishes a thermal-flow requirement. It does not select a pump.
The assumed temperature decrease must be achievable at the required supply temperature and equipment conditions. If users return warmer water than expected, more circulation may be needed to transfer the same heat.
For glycol mixtures or other fluids, use properties appropriate to the actual composition and temperature.
Pump Head Comes from the Operating Network
The pump must deliver the required flow against the resistance of the applicable network.
For parallel users, evaluate the common header and each active branch. The controlling branch can change when different combinations operate.
Review:
- Supply and return piping losses
- Exchanger and jacket characteristics
- Control-valve pressure requirements
- Minimum equipment flow
- Low-demand operation and pump control
- Suction conditions and system pressurization
Do not add the pressure losses of parallel branches as though the entire flow passes through them in series.
Likewise, a heat-duty total does not identify valve size. Each branch needs its own flow range, pressure conditions, and control assessment.
These are engineering deductions from the network arrangement, rather than specifications for a particular packaged system.
Cleaning Demand Needs Its Own Schedule
Cleaning-in-place, or CIP, is a useful example of an intermittent utility user.
Tetra Pak’s cleaning handbook describes CIP stations as systems for storing, monitoring, and distributing cleaning fluids to different circuits. The chapter concerns dairy processing; its relevant lesson here is that cleaning involves coordinated circuits and equipment. (dairyprocessinghandbook.tetrapak.com)
Alfa Laval’s brewery CIP description identifies successive cleaning phases and adjustable time, temperature, pressure, and flow conditions. A real recipe must be established for the product, soil, equipment, and required cleaning outcome. (alfalaval.com)
Consequently, do not assign one constant utility demand to an entire cleaning cycle without checking its phases.
Also distinguish utility circulation from cleaning-fluid return. Alfa Laval identifies entrained-air handling as a consideration in its CIP-return pump application description. That duty should not automatically inherit the assumptions used for a fully flooded hot-water circulation pump. (alfalaval.us)
What to Put in the Utility Design Basis
A useful design basis should let another engineer reproduce the selection.
Record each user’s demand, duration, temperature requirements, and permitted operating combinations. State whether values are measured, supplier-provided, or estimated.
Then identify:
- Normal production and cleaning scenarios
- Startup and recovery cases
- Scheduling restrictions
- Storage assumptions, if applicable
- Distribution losses and explicit design allowances
- Future expansion requirements
- Conditions for performance testing
During commissioning, measure temperatures, flows, and relevant pressures while representative users operate together. Comparing only daily energy consumption with the estimate cannot demonstrate satisfactory peak performance.
Frequently Asked Questions (FAQ)
Can I apply a standard diversity factor to every batch plant?
No universal factor follows from this example. Any reduction needs a defensible operating basis.
Does thermal storage remove the need to check peak demand?
No. Check usable stored energy, delivery rate, temperature limits, and recharge time.
Should the utility pump handle every user’s maximum flow simultaneously?
Assess the operating combinations that the design must support, including credible recovery and startup cases.
Does meeting the calculated flow guarantee heating time?
No. Supply temperature, exchanger performance, control behavior, and process conditions also matter.
Conclusion
Batch utility sizing is a timing problem as well as a capacity problem.
Build the load schedule, distinguish peak demand from average consumption, and test the assumptions behind non-simultaneous operation. Then connect thermal requirements to branch flows, pump duty, valves, and commissioning evidence.
Sources
- KHS — Innoplant: From Initial Idea to Turnkey Beverage Plant and Beyond. Manufacturer announcement, November 2, 2026.
- Spirax Sarco — Methods of Estimating Steam Consumption. Manufacturer engineering guidance; publication date not stated.
- Tetra Pak — Cleaning of Dairy Equipment. Manufacturer technical handbook; chapter revision date not verified.
- Alfa Laval — CIP Station. Manufacturer application description; publication date not stated.
- Alfa Laval — Self-Priming BioPharm Pump Application. Used for the entrained-air CIP-return duty; publication date not stated.
Sources checked November 3, 2026. Calculations are illustrative. No universal sizing margin, cleaning recipe, or new standard requirement is asserted.